
 EN




Choosing the correct press tooling is one of the most consequential decisions a tablet manufacturer can make. The right press tooling directly influences tablet weight consistency, hardness, surface finish, and overall production efficiency. Whether you operate a small-batch nutraceutical facility or a high-volume pharmaceutical plant, the quality and compatibility of your press tooling will shape every tablet your machines produce. A poor choice leads to premature wear, capping defects, and costly downtime, while a well-matched selection drives reliable output and longer equipment life.
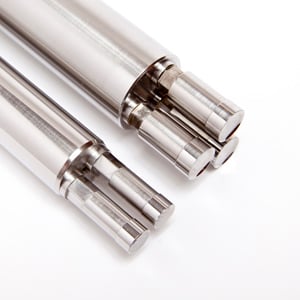
This guide walks tablet makers through the most important considerations when selecting press tooling. From understanding tooling standards and material grades to evaluating cup depth and surface coatings, each factor plays a specific role in final tablet quality. By the end, you will have a structured framework for evaluating press tooling options with confidence and technical clarity.
Understanding Press Tooling Standards and Compatibility
Why Tooling Standards Matter for Tablet Presses
Press tooling is manufactured to industry-recognized standards, most commonly TSM and EU formats. TSM, or Tablet Specification Manual, is widely used in North America, while EU standard press tooling is more common across European pharmaceutical operations. Choosing press tooling that does not match your tablet press machine standard results in poor punch seating, uneven compression forces, and potential equipment damage. Before evaluating any other factor, confirm which standard your press requires and source press tooling accordingly.
Beyond the basic standard, press tooling also comes in different sizes such as B, D, and BB types. Each size determines the maximum tablet diameter and the compression force the punch can safely handle. Matching press tooling size to your formulation and target tablet dimensions is not optional — it is a foundational compatibility requirement that affects every downstream process variable.
Verifying Dimensional Tolerances in Press Tooling
High-precision press tooling must meet tight dimensional tolerances to function correctly within rotary tablet presses. Tolerances in punch barrel diameter, tip diameter, and overall length must align with the press manufacturer's specifications. When press tooling deviates even slightly from the required dimensions, it creates uneven tablet weight and accelerates die bore wear. Always request dimensional inspection reports from your press tooling supplier before committing to a production run.
Selecting the Right Material and Coating for Press Tooling
Steel Grades Used in Press Tooling Manufacturing
The steel grade of press tooling determines its hardness, corrosion resistance, and suitability for specific formulations. Standard press tooling is commonly made from S7 tool steel or the equivalent EN X153CrMoV12 grade, which offers a good balance of toughness and wear resistance for general pharmaceutical applications. For highly abrasive formulations, press tooling made from high-speed steel or carbide-tipped punches offers superior longevity. Corrosive or moisture-sensitive compounds may require stainless steel press tooling or additional protective coatings to prevent oxidation and product contamination.
Understanding the chemistry of your tablet formulation before selecting press tooling material is essential. Abrasive excipients such as dicalcium phosphate accelerate tip wear rapidly, while sticky compounds like certain APIs cause punch tip adhesion. Matching press tooling material to formulation characteristics prevents premature failure and reduces the frequency of tool replacement cycles.
Surface Coatings That Extend Press Tooling Performance
Modern press tooling is frequently enhanced with specialized surface coatings that improve release properties, reduce sticking, and extend service life. Common coatings applied to press tooling include chrome, electroless nickel, titanium nitride, and DLC or diamond-like carbon. Each coating offers a distinct trade-off between hardness, smoothness, and chemical compatibility with tablet ingredients. Chrome-coated press tooling is a durable general-purpose option, while DLC-coated press tooling excels in anti-stick performance for hygroscopic or high-fat formulations. Selecting the appropriate coating for your specific product family reduces tablet picking, sticking, and filming defects significantly.
Evaluating Cup Depth, Embossing, and Tablet Design Factors
How Cup Depth Affects Tablet Quality in Press Tooling
Cup depth in press tooling refers to the concave shape machined into the punch tip face, and it directly controls tablet thickness and volume. Standard, deep, and extra-deep cup configurations in press tooling each produce different tablet profiles. A deeper cup in press tooling creates a more domed tablet with greater volume, which affects disintegration time and patient swallowability. Press tooling with a shallow or flat cup produces flatter tablets suitable for film-coating operations. Selecting the correct cup geometry in your press tooling requires alignment between your formulation bulk density, target fill weight, and the mechanical limits of your tablet press.
Tablet producers must also consider the relationship between cup depth and ejection forces. Deep-cup press tooling can generate higher ejection resistance, especially with sticky formulations, which increases wear on the lower punch and die. When selecting press tooling with a specific cup configuration, always model the expected ejection force against your press machine's rated capacity to avoid mechanical stress.
Embossing and Logo Integration in Press Tooling Design
Custom embossing is a common requirement in pharmaceutical and nutraceutical press tooling. Characters, logos, score lines, and break notches are all machined directly into the press tooling tip face. The depth, font style, and edge sharpness of embossed features on press tooling affect sticking tendencies and tablet defect rates. Fine or intricate designs on press tooling tips are more prone to product buildup and require more frequent cleaning cycles. When specifying embossing details on press tooling, choose bold, clean geometries with smooth transitions and adequate draft angles to minimize adhesion and facilitate clean tablet release from the press tooling surface.
FAQ
What is the difference between TSM and EU press tooling standards?
TSM press tooling and EU press tooling differ primarily in punch barrel dimensions and tip geometry tolerances. TSM press tooling is the standard used in North American tablet press equipment, while EU press tooling follows specifications common in European machinery. Using press tooling from the wrong standard on a given press can cause mechanical incompatibility and increase the risk of punch breakage or uneven tablet weight.
How often should press tooling be inspected or replaced?
Press tooling should be inspected dimensionally after every production campaign and thoroughly before each new product run. Replacement frequency for press tooling depends on abrasiveness of the formulation, compression force levels, and coating condition. As a practical guideline, press tooling showing measurable tip wear beyond tolerance limits, visible pitting, or coating degradation should be retired immediately to prevent tablet quality failures and press damage.
Can press tooling be refurbished instead of replaced?
Yes, press tooling can often be refurbished through professional reconditioning services that include re-polishing punch tips, re-applying surface coatings, and re-checking dimensional tolerances. Refurbished press tooling offers a cost-effective alternative to full replacement, particularly for punches with minimal core wear. However, press tooling with cracks, significant barrel scoring, or deformed tips should never be refurbished, as these defects compromise tablet integrity and press machine safety under high compression forces.