
 EN


Factory productivity hinges on equipment reliability, and punching operations represent a critical bottleneck in metal fabrication workflows. The lifespan of punching dies directly impacts production costs, downtime frequency, and overall operational efficiency. Understanding how to maximize punching performance and durability is essential for any facility managing high-volume stamping or forming processes. This article explores practical strategies to extend punching die service life, reduce replacement frequency, and maintain consistent quality across your factory lines.
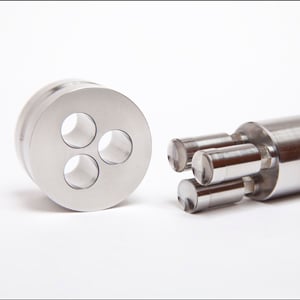
Extending punching die service life requires a comprehensive approach combining proper maintenance, material selection, operational discipline, and predictive monitoring. Factory managers and tooling specialists who implement these strategies report significant reductions in tool wear, improved edge quality, and extended intervals between die replacement cycles. The investment in preventive care typically pays for itself within months through reduced scrap rates and minimized production interruptions.
Optimizing Punching Die Maintenance Protocols
Establishing Routine Cleaning and Inspection Schedules
Regular cleaning directly impacts punching die longevity by removing metal debris, oils, and contaminants that accumulate during production cycles. Each shift should include a brief inspection where operators check for visible damage, unusual wear patterns, or material buildup on the punching surfaces. Debris trapped between die components accelerates wear and reduces cut quality, making scheduled cleaning sessions non-negotiable for maintaining punching performance. Implementing a daily cleaning log ensures accountability and creates a historical record that helps identify recurring issues before they cause catastrophic failures.
Applying Appropriate Lubricants and Coolants
The choice of lubricant significantly influences how well your punching dies resist wear and thermal stress. Industrial facilities should select lubricants specifically formulated for punching applications, as these reduce friction between the die and workpiece while dissipating heat generated during impact. Applying coolant at the point of punching operation extends die service life by maintaining optimal temperatures and preventing premature hardness loss. However, excessive lubrication can attract abrasive particles, so moderation and precision in application are critical. Technicians should replace coolants on a scheduled basis rather than allowing buildup of degraded or contaminated fluids that could damage punching precision.
Material Handling and Operational Best Practices
Controlling Workpiece Material Quality and Feed Consistency
The hardness and surface condition of incoming materials directly influence punching die stress and wear rates. Factory lines should implement incoming material inspection procedures to verify that workpiece specifications match die design tolerances. Inconsistent material properties force punching dies to work under uneven stress conditions, accelerating localized wear and edge degradation. Surface contamination, scale, or oxidation on raw materials can cause abrasive damage during punching operations, so adequate material preparation is essential. Coordinating with suppliers to maintain consistent material grades reduces the variability that shortens punching die service life.
Monitoring Press Alignment and Die Mounting Pressure
Misaligned punching equipment creates uneven load distribution across die surfaces, causing premature edge failure on one side while the opposite side remains underutilized. Factory technicians should verify that all punching press components maintain proper alignment according to equipment specifications. Incorrect mounting pressure or worn mounting fixtures allow die shifting during operation, which exacerbates edge chipping and creates inconsistent hole geometry. Investing in precision mounting blocks and regular press calibration protects punching dies from mechanical damage that could be avoided through simple preventive maintenance. Load cells and pressure sensors provide real-time data to alert operators when punching conditions drift outside acceptable ranges.
Advanced Monitoring and Predictive Replacement Strategies
Implementing Edge Quality Assessment and Predictive Analytics
Modern factories leverage visual inspection systems and sample part analysis to track gradual degradation in punching performance before catastrophic failure occurs. Monitoring burr height, edge roundness, and surface finish provides early warning signals that punching dies are approaching end-of-life. Statistical process control charts document how quality metrics change over production runs, enabling technicians to predict optimal replacement timing rather than reacting to failures. Predictive maintenance reduces unplanned downtime by scheduling punching die replacement during planned maintenance windows rather than mid-shift emergencies.
Tracking Cycle Counts and Establishing Replacement Intervals
Each punching operation increments the total cycle count on a die, and maintaining detailed records enables data-driven replacement decisions. Factory systems should log the number of parts processed through each punching station, correlate this data with quality metrics, and establish baseline service life expectations for different material types and thicknesses. Comparing actual performance against historical averages helps identify dies that underperform or environmental factors degrading service life prematurely. Scheduling proactive punching die replacement based on cycle data and quality trends prevents sudden quality drops and maintains customer satisfaction with consistent part specifications.
FAQ
What factors most significantly reduce punching die service life?
Material contamination, misaligned press equipment, excessive impact velocity, inadequate coolant application, and thermal stress from friction are the primary culprits shortening punching die life. Workpiece material inconsistency compounds these issues by forcing punching dies to adapt to varying hardness and surface conditions. Operator error and improper die mounting add mechanical stress that accelerates wear beyond normal expectations for that punching application.
How often should punching dies be professionally maintained or reworked?
Maintenance frequency depends on production volume, material types, and punching complexity, but most industrial facilities benefit from professional reworking every 50,000 to 200,000 cycles. Smaller production runs may justify less frequent punching die servicing, while high-speed automated lines should schedule professional inspection and edge re-honing every 4 to 8 weeks. Professional technicians can restore dulled edges, address minor damage, and extend overall service life by 30 to 50 percent compared to running punching dies until complete failure.
Can changing material supplier improve punching die service life?
Yes, inconsistent material quality is a common hidden factor reducing punching die life. If incoming workpieces vary significantly in hardness, surface finish, or chemical composition, changing suppliers or establishing stricter material specifications can immediately extend die service life. Working with suppliers willing to provide material certifications and tighter tolerances ensures your punching equipment operates under stable, predictable conditions that maximize die longevity and minimize premature wear.